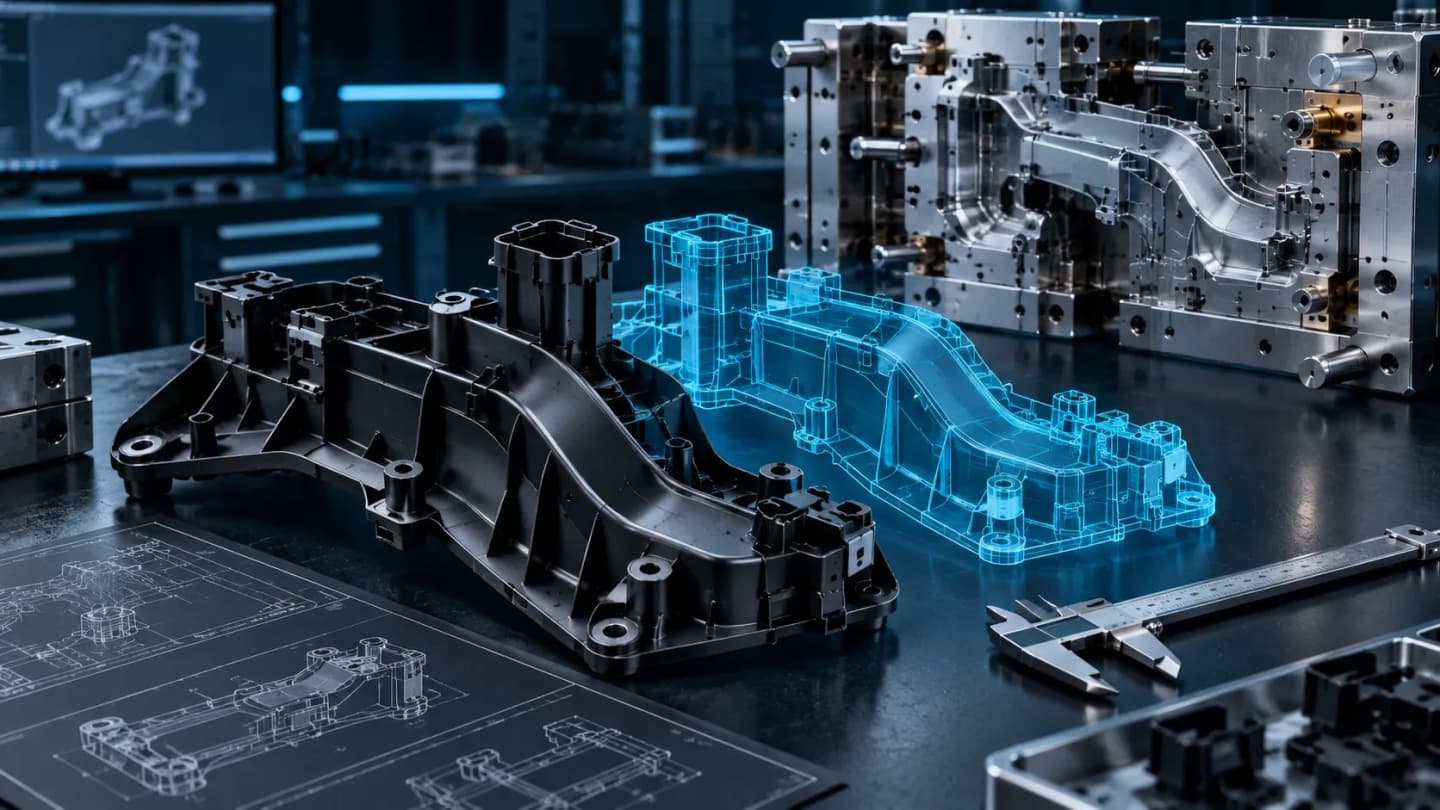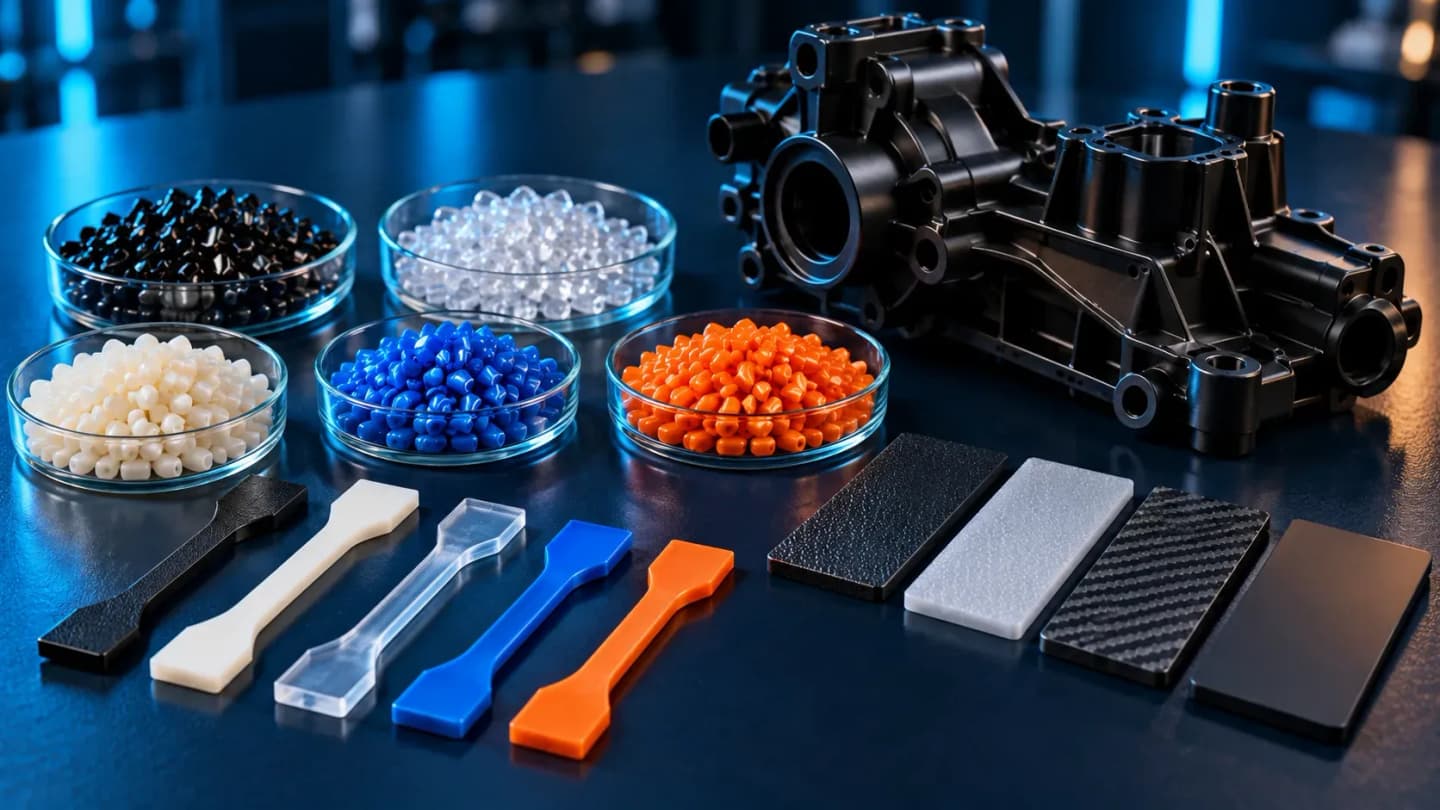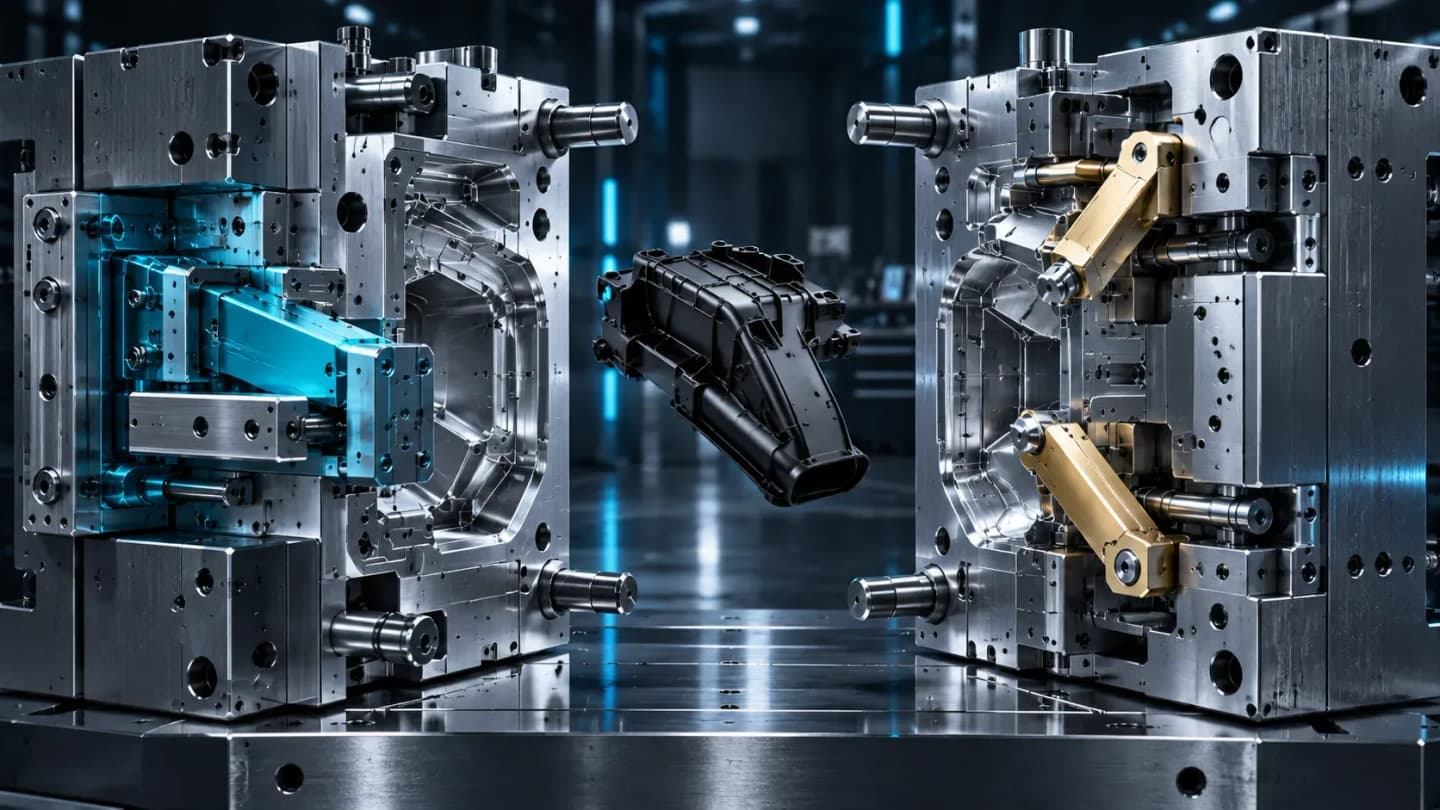
Core, cavity and parting line
The core generally forms internal features while the cavity forms the outer profile, although the practical split depends on part retention and ejection. The parting line is the boundary where the mould halves meet and often leaves a visible witness on the component.
Gate, runner and vent
The runner carries melt from the machine nozzle toward the cavity; the gate is the controlled entry into the part. Vents allow displaced air and process gases to escape at the end of fill without allowing unacceptable flash.
Slider, lifter and ejector
A slider releases a side feature through lateral movement. A lifter combines angled release with the ejection stroke, commonly for internal undercuts. Ejector pins, sleeves or plates then move the moulding away from the core after it has cooled sufficiently.
DFM, trial and validation
Design for manufacturability is the structured review of part geometry and production requirements before tool manufacture. A trial produces controlled sample evidence; validation confirms that agreed dimensional, functional, appearance and process requirements have been met.